About 50 LPH Commercial RO Plant
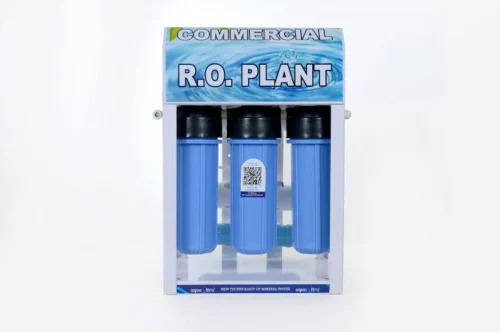
Discover the optimum solution for commercial water purification with our 50 LPH Commercial RO Plant. Engineered for matchless performance, this top-ranking system features a robust FRP structure, powder-coated steel cabinet, and three-stage membrane technology. Designed for easy service, it suits feed water hardness up to 1000 ppm, maintains a controlled inlet flow, and ensures up to 25% water recovery. Advance Purchase is seamless-find, evaluate, and purchase the right plant for your needs. With manual discharge, floor mounting, and low noise operation, experience premium efficiency for your business.
Specific Usage and Key Features: 50 LPH Commercial RO Plant
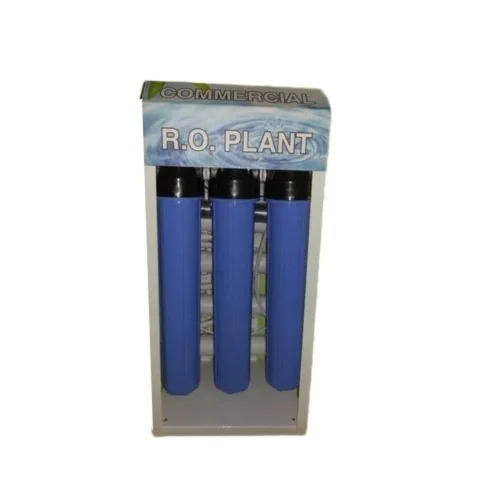
The 50 LPH Commercial RO Plant is engineered for water purification in commercial environments with salt water sources, ensuring consistent water quality with low noise. Its floor-standing design boasts blue cylinders, easy maintenance, and a multi-stage filter system, making it suitable for diverse industries. The high-pressure RO pump paired with FRP material ensures durability and efficiency in water treatment, catering specifically to businesses requiring reliable, top-ranking purification with a 50 LPH flow rate.
Sample Policy, Shipping, and Certification Details
Request a detailed quotation to explore our sample policy, which prioritizes premium customer experience. Samples are shipped from our designated FOB port in India, ensuring efficient order processing for timely deliveries. Our 50 LPH Commercial RO Plant carries industry-standard certifications, guaranteeing quality and compliance. When you purchase, rest assured that both our manufacturing and service teams adhere to strict premium standards, ensuring you receive a top-tier solution for your water purification needs.
FAQ's of 50 LPH Commercial RO Plant:
Q: How does the 50 LPH Commercial RO Plant operate in handling high inlet hardness water?
A: The plant is designed to treat water with inlet hardness up to 1000 ppm, thanks to its multi-stage filtration and robust reverse osmosis membranes, ensuring optimal purification and safe water output.
Q: What specific applications can benefit from this RO Plant's features?
A: This RO Plant is ideal for commercial settings such as manufacturing units, hotels, schools, and hospitals that require purified water continuously with easy maintenance and efficient processing.
Q: When can customers expect sample shipping and order processing after purchase?
A: Once a quotation is approved and the order is confirmed, samples and commercial units are processed promptly, with shipping handled via our FOB port to ensure timely delivery.
Q: Where is the 50 LPH Commercial RO Plant typically installed?
A: The system is designed for floor-mounted installation and is suitable for use in any commercial environment requiring dependable water purification from salt water sources.
Q: What is the process for advance purchase and getting a quotation?
A: Customers can request a quotation directly from our sales team, compare specifications, and proceed with the advance purchase to secure their order. Our team facilitates smooth order placement and provides necessary support throughout the process.
Q: How easy is it to maintain the plant and service its components?
A: The plant is engineered for easy service, enabling routine maintenance and component replacement with minimal downtime, ensuring consistent water treatment performance for users.


 Send Inquiry

 Send Inquiry


